
From Simulation to Winding: Closing the Gap in Custom High-Frequency Transformer Prototypes
People often ask for the best custom transformer manufacturer China. A better question is simpler: best for which job, under whose conditions, and with what proof? For power-electronics engineers and OEM sourcing teams, From Simulation to Winding: Closing the Gap in Custom High-Frequency Transformer Prototypes is a practical guide to that gap. It looks at the awkward details buyers actually inherit: interfaces, variation, training, maintenance and the evidence needed when something changes.
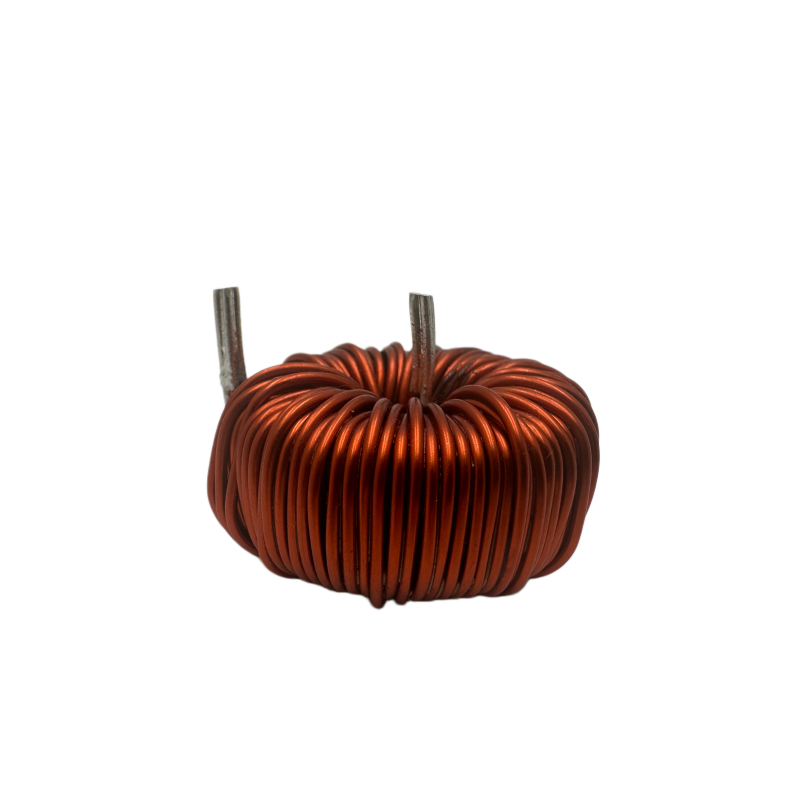
How to test converter waveform and duty cycle without overcomplicating it
Teams tend to notice problems with converter waveform and duty cycle only after the result slips. By then, the cause may be several steps upstream. Run the comparison at the edges of the expected workload, not only at the comfortable centre where almost every option looks good. The practical risk is not a dramatic breakdown. It is a slow drift that people learn to work around until the workaround becomes the process. Price the return to stable operation, not just the purchase. Cleaning, changeover, rejected work and diagnosis time belong in the same calculation. That is a far more useful definition of reliability than a perfect number produced once under ideal conditions.
Start with flux density and core loss, because that is where an otherwise sensible plan can come unstuck. Ask what has to be cleaned, adjusted or replaced after a normal shift. Those routine details are where ownership cost becomes visible. That matters because flux density and core loss and common-mode impedance over frequency are tied together; pushing one harder can simply move the bottleneck. Save the failed sample as carefully as the successful one. It usually explains more about the operating window. If the team cannot repeat the result, it has not finished the test; it has only seen a promising moment.
The part people miss about leakage inductance as a design variable
One small mismatch in leakage inductance as a design variable can quietly shape the rest of a custom transformers, inductors and nanocrystalline chokes project. Record both the setting and the result. A good sample without its conditions is a memory, not evidence. The difference only becomes obvious when volume, material, environment or user behaviour moves away from the demonstration case. Agree on the evidence before the test begins, including who can accept a deviation and what happens to the affected work. This small discipline is often the difference between a manageable variation and a recurring mystery.
Related official resource: Official website
On paper, winding capacitance often looks settled. On the floor, it rarely is. Instead of asking whether it is 'high quality', ask for the tolerance, test method, dated sample or service record that supports the claim. The snag is that thermal rise in enclosure does not wait politely downstream. It feeds back into the decision and changes what 'acceptable' looks like. Check service access and spare-part lead time now. Maintenance that is awkward on day one is likely to be postponed on day one hundred. At the winding capacitance stage, that is a far more useful definition of reliability than a perfect number produced once under ideal conditions.
Put insulation system and creepage into working terms
Ask two suppliers about insulation system and creepage and you may hear two perfectly confident, completely different answers. When reviewing insulation system and creepage, ask what has to be cleaned, adjusted or replaced after a normal shift. At the insulation system and creepage stage, those routine details are where ownership cost becomes visible. What looks like a product issue may actually be an interface issue, which is cheaper to discover before installation than after it. Where safety, compliance or performance is involved, trace the claim back to the exact model, market and operating condition. It also makes the supplier conversation sharper: both sides can discuss a visible condition instead of trading adjectives.
Picture the first busy week after handover: copper loss and skin effect is no longer a brochure claim but a daily constraint. At the copper loss and skin effect stage, ask what has to be cleaned, adjusted or replaced after a normal shift. With insulation system and creepage in view, those routine details are where ownership cost becomes visible. For copper loss and skin effect, the difference only becomes obvious when volume, material, environment or user behaviour moves away from the demonstration case. A short, dated record beats a thick manual nobody opens. It should help the next person make a decision without reconstructing the whole story. With insulation system and creepage in view, if the team cannot repeat the result, it has not finished the test; it has only seen a promising moment.
What the brochure cannot show about thermal rise in enclosure
It is tempting to treat thermal rise in enclosure as a box to tick. That is usually where trouble starts. Write the hand-off in plain language: what arrives, what must happen, what leaves, and what the next person needs from it. The snag is that saturation under imbalance does not wait politely downstream. At the thermal rise in enclosure stage, it feeds back into the decision and changes what 'acceptable' looks like. Keep the proof proportionate: a reversible cosmetic choice needs less control than a hidden interface that can stop the whole operation. A good decision leaves a trail that another person can follow without guessing what the original team meant.
Use the official website to see how TrafoPSU describes its range, then open Current Transformer Manufacturer with a notebook beside you. Do not copy the claims into a specification. Turn them into questions: which model, which test condition, which limit, and who supports the product after delivery? Product pages are useful for narrowing the field. Written confirmation and a trial with the buyer's real conditions are what close the gap.
Related official resource: Current Transformer Manufacturer
Where gap tolerance and acoustic noise starts to matter
The language around gap tolerance and acoustic noise sounds technical, but the decision is often surprisingly ordinary: who checks what, when, and against which limit? For gap tolerance and acoustic noise, record both the setting and the result. When reviewing gap tolerance and acoustic noise, a good sample without its conditions is a memory, not evidence. If leakage inductance as a design variable is left out, the team may approve a strong component that performs poorly as part of the full system. Use ordinary working conditions, then add one or two difficult cases that represent genuine risk rather than an artificial torture test. For gap tolerance and acoustic noise, a good decision leaves a trail that another person can follow without guessing what the original team meant.
Before asking for a better number on common-mode impedance over frequency, ask what that number actually describes. The quickest reality check is to follow one actual job from arrival to hand-off and write down every assumption made along the way. At the common-mode impedance over frequency stage, the practical risk is not a dramatic breakdown. With gap tolerance and acoustic noise in view, it is a slow drift that people learn to work around until the workaround becomes the process. Define the exception path while everyone is calm: stop, segregate, slow down, use an approved substitute or call for technical review. When reviewing common-mode impedance over frequency, if the team cannot repeat the result, it has not finished the test; it has only seen a promising moment.
How to test saturation under imbalance without overcomplicating it
On paper, saturation under imbalance often looks settled. At the saturation under imbalance stage, on the floor, it rarely is. With converter waveform and duty cycle in view, ask what has to be cleaned, adjusted or replaced after a normal shift. For saturation under imbalance, those routine details are where ownership cost becomes visible. When reviewing saturation under imbalance, the difference only becomes obvious when volume, material, environment or user behaviour moves away from the demonstration case. After a few months, compare the original assumptions with throughput, complaints and service notes. Repeated patterns deserve a response; isolated noise may not. For saturation under imbalance, if the team cannot repeat the result, it has not finished the test; it has only seen a promising moment.
The language around sample correlation to simulation sounds technical, but the decision is often surprisingly ordinary: who checks what, when, and against which limit? A clean specification should name the real input, the normal range and the point where the result becomes unacceptable. A supplier may be right under its test conditions and the buyer may still be disappointed under theirs. Both can be true. At the sample correlation to simulation stage, save the failed sample as carefully as the successful one. With copper loss and skin effect in view, it usually explains more about the operating window. For sample correlation to simulation, that is a far more useful definition of reliability than a perfect number produced once under ideal conditions.
Read production winding and test control alongside sample correlation to simulation
Teams tend to notice problems with production winding and test control only after the result slips. For production winding and test control, by then, the cause may be several steps upstream. When reviewing production winding and test control, record both the setting and the result. At the production winding and test control stage, a good sample without its conditions is a memory, not evidence. In custom transformers, inductors and nanocrystalline chokes, the result is rarely controlled by one variable. Sample correlation to simulation can change the meaning of an otherwise impressive figure for production winding and test control. When reviewing production winding and test control, price the return to stable operation, not just the purchase. At the production winding and test control stage, cleaning, changeover, rejected work and diagnosis time belong in the same calculation. With sample correlation to simulation in view, this small discipline is often the difference between a manageable variation and a recurring mystery.
Related official resource: inductors and chokes
One small mismatch in converter waveform and duty cycle can quietly shape the rest of a custom transformers, inductors and nanocrystalline chokes project. When reviewing converter waveform and duty cycle, record both the setting and the result. At the converter waveform and duty cycle stage, a good sample without its conditions is a memory, not evidence. This is why a nominal value should be treated as the start of the conversation, not the end of it. For converter waveform and duty cycle, where safety, compliance or performance is involved, trace the claim back to the exact model, market and operating condition. The point is not more paperwork. It is fewer arguments based on memory after time and money have already been committed.
Turn flux density and core loss into evidence
Before asking for a better number on flux density and core loss, ask what that number actually describes. At the flux density and core loss stage, run the comparison at the edges of the expected workload, not only at the comfortable centre where almost every option looks good. With common-mode impedance over frequency in view, the practical risk is not a dramatic breakdown. For flux density and core loss, it is a slow drift that people learn to work around until the workaround becomes the process. When reviewing flux density and core loss, price the return to stable operation, not just the purchase. At the flux density and core loss stage, cleaning, changeover, rejected work and diagnosis time belong in the same calculation. With common-mode impedance over frequency in view, if the team cannot repeat the result, it has not finished the test; it has only seen a promising moment.
Start with leakage inductance as a design variable, because that is where an otherwise sensible plan can come unstuck. Put the operator, buyer and supplier around the same sample. Their different questions usually reveal gaps that a feature table cannot. When reviewing leakage inductance as a design variable, the difference only becomes obvious when volume, material, environment or user behaviour moves away from the demonstration case. At the leakage inductance as a design variable stage, define the exception path while everyone is calm: stop, segregate, slow down, use an approved substitute or call for technical review. With flux density and core loss in view, that is a far more useful definition of reliability than a perfect number produced once under ideal conditions.
A Decision That Can Be Defended
There is no magic checklist for custom transformer manufacturer China. There is, however, a dependable habit: describe the real job, test the awkward case, keep the setting with the result, and decide who owns the next step. Do that and the team can live with normal variation without mistaking it for failure. More importantly, it can spot the abnormal variation early. That is what turns a purchase from a confident guess into a decision that still holds up after handover.
Рассказать о статье
Последние публикации
-
 Інвертор 2 чи 3 кВт: як знайти оптимальний варіант для дому та техніки Сентябрь 12, 2026
-
 Чисті вікна до блиску: чому варто довірити миття професіоналам Сентябрь 10, 2026
-

-

-
 Скляні двері та перегородки loft: як зберегти світло між кімнатами Сентябрь 1, 2026
-
 Популярні напрямки та готелі, які варто розглянути Август 26, 2026
-

-

-
 Как резиновые коврики могут защитить багажник машины? Август 20, 2026